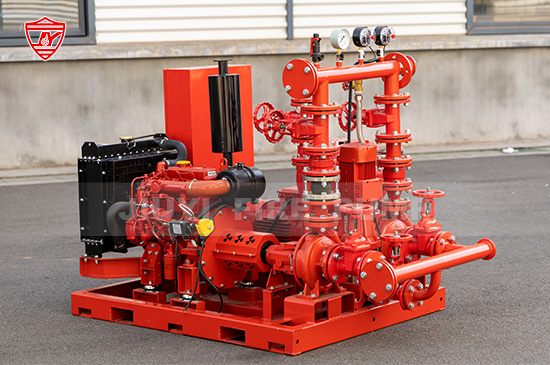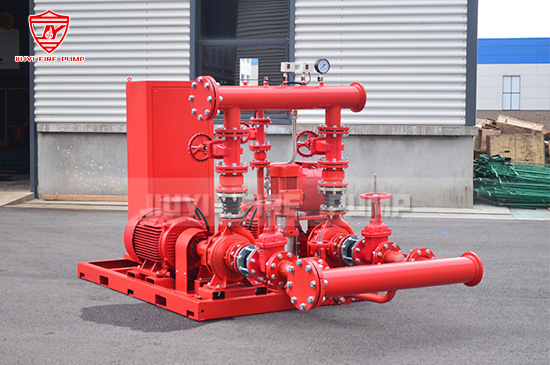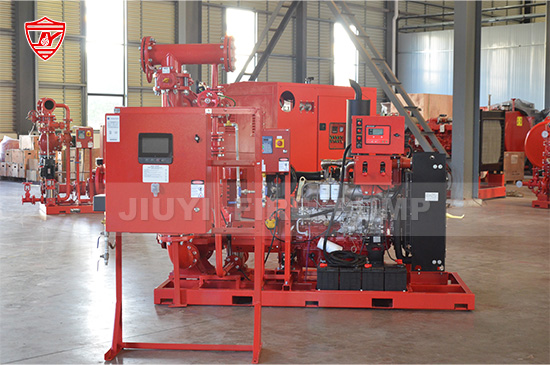
Fire pumps are critical components of fire protection systems, but their operating and maintenance costs can add up over the life of a facility. Energy consumption, routine maintenance, testing, spare parts, fuel, and unexpected repairs can all contribute to the total cost of ownership.
For building owners, fire protection contractors, system designers, and facility managers, reducing these costs does not mean compromising fire safety. In fact, a properly designed, correctly sized, and well-maintained fire pump system can improve reliability while controlling long-term operating expenses.
The key is to look beyond the initial purchase price and consider the complete lifecycle of the fire pump system.
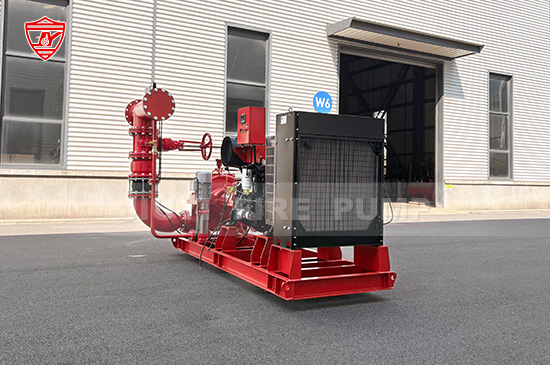
One of the most effective ways to control fire pump operating costs is to select the right pump from the beginning.
A fire pump should be selected according to the required flow, pressure, system demand, suction conditions, and applicable fire protection requirements. Choosing a pump that is significantly oversized can increase equipment costs and may result in inefficient operation when the system frequently operates away from its intended duty point.
At the same time, selecting a pump that is too small can prevent the system from delivering the required fire flow and pressure.
The objective is to match the fire pump performance curve with the actual hydraulic requirements of the fire protection system.
When selecting a pump, consider:
Required rated flow
Required rated pressure
System demand
Suction pressure
Elevation and friction losses
Operating conditions
Motor or diesel engine requirements
Applicable certification and approval requirements
Future system requirements
Proper selection helps avoid unnecessary energy consumption and reduces the possibility of premature equipment problems.
The efficiency of the pump itself is only one part of the overall system.
Piping, valves, fittings, strainers, elbows, check valves, and other components create hydraulic resistance. Excessive friction losses require the pump to generate additional pressure, which can increase energy consumption.
A well-designed fire protection system should minimize unnecessary pressure losses while maintaining the required fire protection performance.
During system design or modification, engineers should evaluate pipe sizing, pipe routing, fitting arrangements, valve selection, and other hydraulic factors.
For existing installations, unusual pressure losses can sometimes indicate problems such as partially closed valves, blocked strainers, damaged components, or changes in system conditions.
Maintaining good hydraulic performance can help the fire pump operate closer to its intended duty point.
Oversizing is a common consideration when evaluating fire pump lifecycle costs.
A larger pump does not automatically mean a better fire protection system. The pump must meet the required fire demand, but excessive capacity can increase the size and cost of the motor, controller, electrical infrastructure, piping, and related equipment.
For electric fire pumps, unnecessary capacity may also result in higher electrical demand when the pump operates.
For diesel fire pumps, a larger engine may increase fuel consumption and maintenance requirements.
Fire pump selection should therefore be based on hydraulic calculations and the actual requirements of the project rather than simply selecting the largest available pump.
The correct approach is to provide sufficient performance without unnecessarily increasing the size of the complete system.
The choice between an electric motor and diesel engine driver can affect long-term operating costs.
Electric fire pumps generally have different operating cost characteristics from diesel-driven systems. Electricity availability, local utility rates, standby power requirements, installation conditions, and project requirements should all be considered.
Diesel fire pumps require additional attention to fuel, batteries, engine oil, filters, cooling systems, exhaust systems, and other engine-related components.
Although a diesel fire pump may operate infrequently under normal conditions, its engine must remain ready for emergency operation. Regular inspections and maintenance are therefore essential.
When selecting a driver, consider not only the purchase price but also installation, testing, maintenance, fuel or electricity consumption, spare parts, and expected service life.
Pump efficiency directly influences the energy required to move water.
A well-designed fire pump uses hydraulic components that are engineered to deliver the required flow and pressure effectively. Manufacturing quality, impeller design, casing design, clearances, materials, and production accuracy can all influence pump performance.
The motor or engine should also be properly matched to the pump.
For electric systems, the motor should provide sufficient power for the complete operating range without creating unnecessary inefficiencies. For diesel systems, the engine should be appropriately matched to the pump load and operating requirements.
Because fire pumps are safety equipment, efficiency should always be considered together with required fire protection performance and applicable standards.
Preventive maintenance is one of the most practical ways to control long-term fire pump costs.
Small problems can become expensive failures when they are not identified early. Regular inspection and maintenance help detect developing issues before they affect pump reliability.
Depending on the equipment and applicable requirements, maintenance activities may include checking:
Pump bearings
Shaft alignment
Coupling condition
Mechanical seals or packing
Valves
Pressure gauges
Controllers
Electrical connections
Batteries
Diesel fuel systems
Engine oil
Cooling systems
Exhaust systems
Pump room conditions
Maintenance should follow the equipment manufacturer's recommendations and the applicable fire protection requirements.
A preventive maintenance program can reduce unexpected downtime, emergency repair costs, and premature replacement.
Alignment between the pump and driver is another important factor in controlling maintenance costs.
Poor alignment can place additional loads on bearings, couplings, shafts, and other components. Over time, this can contribute to vibration, wear, overheating, and premature component failure.
During installation and maintenance, alignment should be checked using appropriate procedures and equipment.
The pump, driver, base, coupling, and related components should be installed according to the manufacturer's requirements.
Correct alignment supports smooth operation and helps extend the service life of mechanical components.
Regular fire pump testing provides an opportunity to verify that the system continues to perform as expected.
Performance testing can reveal changes in flow, pressure, vibration, or other operating characteristics. Comparing current results with previous test data can help identify gradual deterioration.
For example, a reduction in pump performance may indicate hydraulic restrictions, component wear, valve problems, or other issues that require investigation.
Testing also provides valuable operating data for maintenance planning.
A well-maintained record of pump performance can help facility managers identify trends instead of waiting until a major problem occurs.
The environment surrounding a fire pump can influence operating reliability and maintenance costs.
The pump room should be kept clean, accessible, and suitable for the equipment installed there. Moisture, excessive dust, corrosion, poor ventilation, extreme temperatures, and inadequate drainage can create additional problems.
For diesel fire pumps, appropriate ventilation and exhaust arrangements are particularly important.
For electric fire pumps, electrical equipment and controllers should be protected from unsuitable environmental conditions.
A clean and well-maintained pump room makes inspections easier and allows problems to be identified more quickly.
Diesel fire pump systems require additional operating considerations.
Fuel quality and storage conditions should be monitored according to the manufacturer's recommendations and applicable requirements. Poor fuel condition can create problems for the engine and fuel system.
Batteries are also essential components of diesel fire pump systems. Battery condition, connections, charging systems, and starting performance should be checked regularly.
Replacing batteries and other consumable components according to their condition and recommended service intervals can help avoid emergency failures and unnecessary repair costs.
For facilities with diesel fire pumps, maintaining the complete engine system is just as important as maintaining the pump itself.
The initial purchase price is only one part of the cost of a fire pump system.
A lower-cost component may appear attractive during procurement but can become more expensive if it requires frequent replacement, creates maintenance problems, or has limited service life.
When comparing fire pumps, consider the total lifecycle cost, including:
Initial equipment cost
Installation
Energy consumption
Fuel consumption
Routine maintenance
Spare parts
Testing
Repairs
Downtime
Expected service life
Reliable manufacturing processes and consistent quality control can contribute significantly to long-term equipment performance.
For critical fire protection systems, reliability should be evaluated together with cost.
The manufacturer's experience can influence the long-term performance of a fire pump system.
An experienced manufacturer can support customers with pump selection, hydraulic performance, driver matching, system configuration, testing, commissioning, and maintenance recommendations.
Manufacturing capabilities are also important. Proper casting, machining, assembly, painting, testing, and quality control can help ensure that the finished pump performs consistently with its specified characteristics.
For projects requiring certified or listed fire pump equipment, manufacturers should also have the appropriate testing and quality systems to support the required products.
When evaluating different fire pump solutions, it is useful to look at the total cost over the expected service life.
For example, two pumps may have similar purchase prices but different maintenance requirements. Another pump may have a higher initial cost but lower energy consumption or longer component life.
A lifecycle approach considers the complete picture.
The main cost categories include equipment acquisition, installation, energy or fuel, maintenance, spare parts, testing, repairs, and eventual replacement.
This approach allows project owners and engineers to make purchasing decisions based on long-term value rather than initial price alone.
The most important principle is that cost reduction should never compromise the performance or reliability of a fire protection system.
Fire pumps are emergency equipment. Their primary purpose is to provide the required water flow and pressure when a fire protection system demands it.
Therefore, energy savings, maintenance optimization, and equipment cost reductions should always be evaluated within the applicable fire protection requirements.
The goal is not simply to make a fire pump cheaper to operate. The goal is to create a reliable fire pump system that provides the required performance while minimizing unnecessary lifecycle costs.
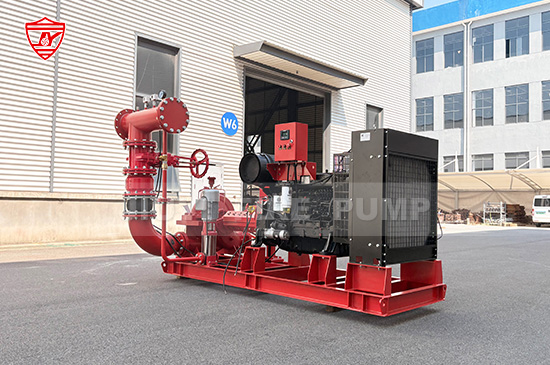
Reducing fire pump operating costs requires a complete approach that starts with proper equipment selection and continues throughout the service life of the system.
Correct pump sizing, efficient hydraulic design, appropriate driver selection, preventive maintenance, regular performance testing, proper alignment, reliable components, and good pump room conditions can all contribute to lower lifecycle costs.
For facility owners, contractors, and fire protection professionals, the most effective strategy is to evaluate the complete fire pump system rather than focusing only on the initial equipment price.
As a fire pump manufacturer, BETTER Technology Group focuses on pump design, manufacturing, testing, and quality control to provide reliable fire pump solutions for different fire protection applications. By combining appropriate pump selection with proper installation and maintenance, customers can achieve a balance between fire protection performance, equipment reliability, and long-term operating costs.
A well-designed and properly maintained fire pump system is not only an inve
stment in fire safety. It is also an investment in predictable operating costs and long-term system reliability.