Fire pump cavitation is a serious hydraulic problem that can reduce pump performance, cause vibration and noise, damage internal components, and compromise the reliability of a fire protection system. Understanding what causes cavitation and how to prevent it is essential for fire pump designers, contractors, maintenance teams, and facility owners.
At the center of the issue is Net Positive Suction Head, commonly known as NPSH. When the pressure available at the pump suction becomes too low compared with the pressure required by the pump, water can begin to vaporize locally. The resulting vapor bubbles can collapse as they move into higher-pressure areas inside the pump, producing shock, vibration, noise, and potentially damaging the impeller and other components.
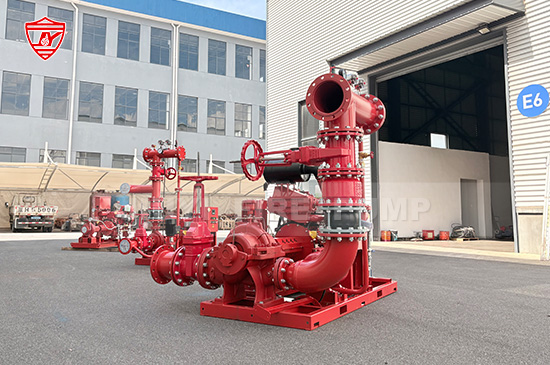
Cavitation occurs when the local pressure of water falls below its vapor pressure. Under these conditions, small vapor bubbles form within the liquid. As the water moves through the pump and pressure increases again, the bubbles rapidly collapse.
This process can be particularly damaging around the impeller eye and other areas where water velocity and pressure change rapidly.
For fire pumps, cavitation is more than an equipment-performance issue. A fire pump is a critical component of a fire protection system and may be required to deliver its rated flow and pressure during an emergency. A pump that has suffered significant cavitation damage may experience reduced hydraulic performance, excessive vibration, or mechanical problems when dependable operation is most important.
Cavitation should therefore be considered during pump selection, hydraulic design, installation, commissioning, testing, and maintenance.
The fundamental issue is insufficient pressure at the pump suction. In engineering terms, the available Net Positive Suction Head can become lower than the Net Positive Suction Head required by the pump.
Several conditions can contribute to this problem:
A cavitation problem can therefore originate outside the pump itself. The pump may be correctly manufactured and tested, while the installed system creates conditions that do not provide sufficient suction pressure.
Two important terms must be understood when evaluating fire pump cavitation: NPSHA and NPSHR.
NPSHA represents the suction head actually available to the pump under the operating conditions of the system.
It depends on factors such as:
Because these factors are determined largely by the system design and installation, NPSHA is strongly influenced by the project conditions.
NPSHR represents the suction head required by a particular pump at a specific operating condition. It is determined from pump performance data and varies with pump design, speed, and flow.
As pump flow increases, NPSHR can also increase. This is particularly important when evaluating a fire pump at high-flow operating conditions.
The basic relationship is straightforward:
NPSHA should be greater than NPSHR under the applicable operating conditions.
NFPA 20 materials identify NPSH supplied and NPSH required as important considerations for fire pump installations. The available suction condition must provide the pump with sufficient NPSH for the specified operating conditions.
The exact design requirements and applicable safety margins should always be determined according to the edition of the applicable fire protection standard, local regulations, project specifications, and the pump manufacturer's requirements.
A fire pump may experience reduced suction pressure when the water level in the supply tank falls.
This can become especially important during a prolonged fire event. The initial water level may appear adequate during normal inspection, but the available head can change as water is consumed.
For this reason, fire pump hydraulic calculations should consider the relevant minimum water level rather than relying only on the normal operating level.
When a pump is installed above its water source, the vertical distance between the pump and water level can reduce the pressure available at the pump suction.
The greater the suction lift, the greater the potential reduction in NPSHA.
Pump location should therefore be considered during the early stages of fire protection system design rather than after the building and water-storage arrangement have already been finalized.
Suction piping that is too small can produce excessive water velocity and friction losses.
These losses reduce the pressure available at the pump inlet. A system may therefore have an adequate water source but still experience insufficient NPSHA because of the suction piping arrangement.
Suction pipe diameter, length, fittings, valves, and configuration should all be considered during hydraulic design.
Elbows, reducers, valves, and other fittings can introduce additional pressure losses and disturb the flow entering the pump.
Poor inlet conditions can be especially problematic when fittings are installed too close to the pump suction.
A well-designed suction arrangement should provide stable and uniform flow into the pump while minimizing unnecessary hydraulic losses.
A suction pipe that was correctly designed can still develop cavitation problems if it becomes restricted.
Potential causes include:
Maintenance teams should therefore inspect the entire suction path when investigating unexplained pump noise, vibration, or loss of performance.
Water temperature affects vapor pressure. As water temperature increases, the pressure required to prevent vapor formation also changes.
This means that a system operating normally under one set of conditions may have a reduced cavitation margin under higher-temperature conditions.
Temperature should therefore be considered when evaluating NPSH, particularly for installations exposed to hot environments or significant seasonal temperature changes.
Fire pumps are designed to operate at specified speeds. Increasing pump speed changes the hydraulic operating conditions and can increase the pump's NPSH requirement.
Incorrect motor frequency, driver settings, or diesel engine speed can therefore contribute to hydraulic problems.
During commissioning and troubleshooting, pump speed should be verified against the approved pump and driver data.
Recognizing cavitation early can help prevent more serious damage.
Typical warning signs include unusual noise, vibration, unstable pressure, reduced flow, and declining pump performance.
A cavitating centrifugal pump may produce a sound similar to gravel or stones moving through the pump. This is caused by the formation and collapse of vapor bubbles.
Other signs may include:
However, these symptoms are not exclusive to cavitation. Similar symptoms can result from air entering the suction line, mechanical problems, improper alignment, or other hydraulic conditions.
For this reason, cavitation should be diagnosed using operating data rather than relying only on sound or vibration.
The most effective approach is to address cavitation during system design.
The selected fire pump should meet the required flow and pressure while operating within the manufacturer's specified hydraulic range.
Pump curves should be reviewed together with NPSH requirements. It is not sufficient to consider only rated flow and rated pressure.
The suction system should minimize unnecessary friction losses and provide suitable flow conditions at the pump inlet.
Consider:
The objective is to maintain sufficient suction pressure throughout the required operating range.
The water source must provide the required quantity of water under the relevant operating conditions.
For tank-fed systems, the lowest expected operating water level should be considered. For other water supplies, changes in available pressure and flow should also be evaluated.
The fire pump should operate at its specified rated speed.
For electric fire pumps, verify the electrical supply and motor operating conditions. For diesel-driven fire pumps, verify engine speed and associated controls.
Maintenance should not focus only on the pump itself.
The complete suction path should be inspected for restrictions, closed or partially closed valves, debris, air leakage, and other conditions that can reduce suction performance.
Fire pump testing provides an opportunity to identify changes in pump behavior.
If the pump develops unusual vibration or noise, produces unstable pressure, or fails to achieve expected performance, the suction conditions should be investigated rather than assuming the pump itself is defective.
Fire pump manufacturers play an important role in reducing cavitation risk through pump hydraulic design, performance testing, and application support.
A reliable manufacturer should be able to provide appropriate pump performance information, including flow, pressure, speed, and relevant NPSH data.
Factory testing can also help verify that the pump performs according to its intended hydraulic characteristics before shipment.
However, factory performance does not guarantee that an installed system will never experience cavitation. Actual field conditions can differ from factory conditions. Water level, suction piping, temperature, elevation, fittings, and operating conditions all influence the hydraulic environment in which the pump operates.
This is why communication between the pump manufacturer, system designer, installer, and project owner is essential.
When cavitation is suspected, begin with the simplest possible checks and work toward a complete hydraulic evaluation.
Check the following:
A systematic approach is more effective than replacing pump components without identifying the underlying cause.
Fire protection systems are designed around reliability. A fire pump may remain idle for long periods and then be required to start and deliver its specified performance immediately.
Cavitation can progressively damage hydraulic components even when the pump continues to operate. If the problem is ignored, the resulting erosion, vibration, and performance deterioration can become increasingly serious.
The best strategy is prevention.
Proper pump selection, accurate hydraulic calculations, suitable suction piping, adequate water supply, correct installation, commissioning, and regular inspection all contribute to reliable fire pump operation.
Fire pump cavitation is fundamentally a hydraulic problem, but its consequences can become mechanical and operational. The key is understanding the relationship between NPSH available and NPSH required.
A fire pump needs adequate suction conditions to convert the available water supply into the required flow and pressure. When suction pressure becomes too low, vapor bubbles can form and collapse inside the pump, potentially causing noise, vibration, erosion, and loss of performance.
For designers and contractors, cavitation prevention begins with the water source, pump selection, and suction piping design. For maintenance teams, it means monitoring pump performance and investigating abnormal noise, vibration, pressure fluctuations, or reduced flow before damage becomes severe.
Choosing a properly engineered fire pump and working closely with the manufacturer during selection and system design can significantly reduce the risk of cavitation and help maintain dependable fire protection performance throughout the life of the system.